
By Propack Technologies / India's Leading Pharma Equipment Supplier & Manufacturing machines
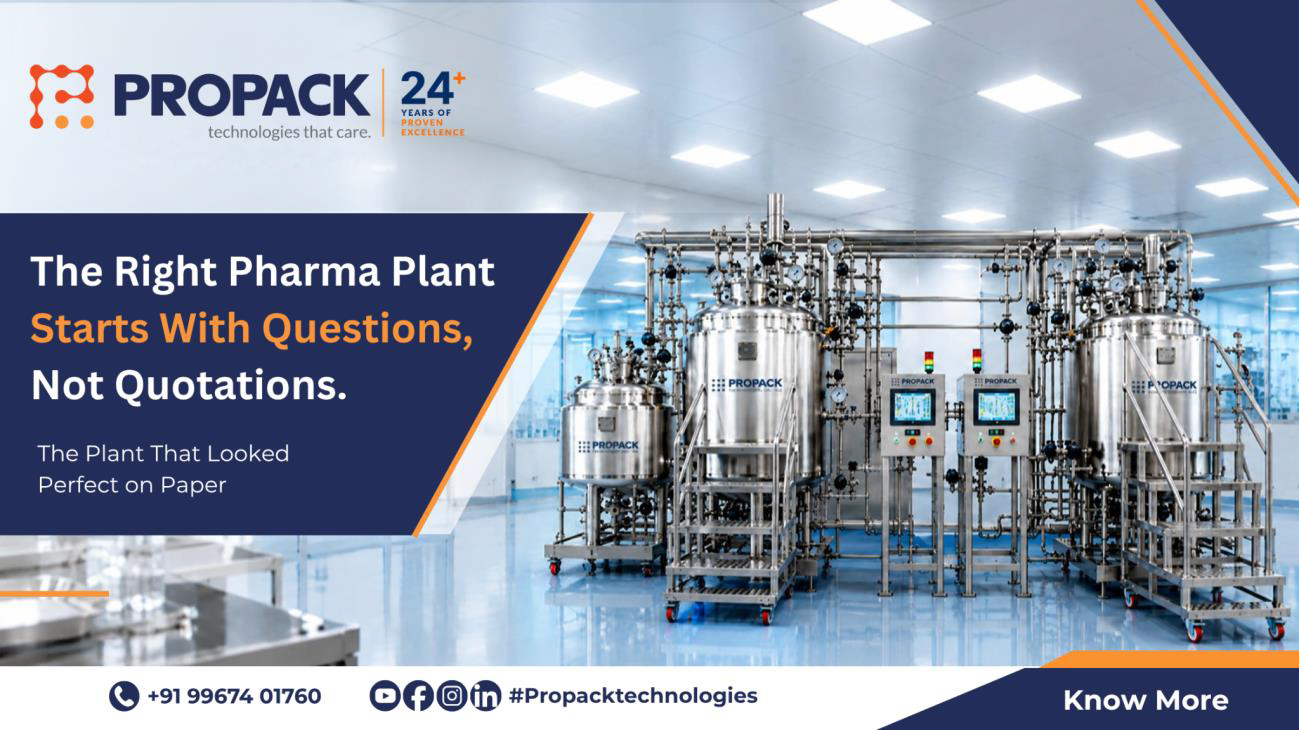
The Plant That Looked Perfect on Paper
Every pharmaceutical manufacturer has seen it happen: a plant gets built, the equipment is top-of-the-line, the fabrication is flawless, and six months later, the team is fighting bottlenecks, failed validations, or a process that simply can't scale the way the business needs it to.
The uncomfortable truth is that most of these problems aren't equipment problems. They're planning problems. By the time a machine is fabricated and installed, the decisions that actually determine whether a plant performs well have already been made, weeks or months earlier, at the engineering table.
A successful pharmaceutical manufacturing plant isn't simply a collection of equipment. It's the outcome of decisions made long before a single vessel is welded: decisions about process flow, automation, validation, and scale. Get those right, and the equipment does its job. Get them wrong, and no amount of stainless steel can fix it later.
So before you finalize your next plant or expansion, here are five questions worth sitting with.
Q1) Does Your Equipment Know What Product It's Making?
It's tempting to think of equipment selection as a catalog exercise: pick a mixer, pick a reactor, pick a filling line. But not every formulation behaves the same way under heat, shear, or agitation. A mixing approach that works beautifully for one product can degrade another. A homogenization method that's gentle enough for a sensitive API might be too slow for a high-viscosity batch.
The question to ask isn't "what equipment do we need?" It's "what does our process actually require, and which equipment is built around that?" When equipment is chosen to fit the process, rather than the process being forced to fit whatever equipment was available, you get better yields, fewer reworks, and a system that behaves predictably batch after batch.
Q2) Process Flow: The Layout Decision That Shapes Plant Efficiency
A plant can have excellent individual machines and still underperform, simply because of how those machines are connected. Piping runs that are longer than they need to be. Utilities positioned as an afterthought. Equipment placed for convenience during construction rather than for efficiency during operation.
Material flow, piping, utilities, and equipment positioning all compound over time. A few extra meters of pipe or an awkwardly placed CIP skid might seem trivial on a drawing, but multiplied across thousands of batches, it becomes lost time, added contamination risk, and higher operating cost. Optimizing flow isn't a nice-to-have; it's one of the few decisions that pays dividends for the entire lifetime of the plant.
Q3) Automation Works Best When It's Part of the Original Design
Automation added as an afterthought rarely performs the way automation designed in from the start does. When the automation strategy is considered alongside the mechanical design, not after it, it becomes possible to build in the consistency, traceability, and control that regulators and operators both expect.
This is also where a lot of future headaches get avoided. Retrofitting automation onto a system that wasn't designed for it usually means compromises: sensors placed where they weren't intended to go, control logic working around mechanical limitations instead of enhancing them. Planning automation early isn't about adding complexity; it's about giving the plant a nervous system that actually fits its body.
Q4) Building a Plant That's Ready for Validation From the Start
Documentation, qualification, and compliance are too often treated as the final hurdle before a plant goes live, something to sort out once construction is done. But validation-readiness isn't a checklist you complete at the end. It's a mindset that needs to run through engineering from the very first drawing.
A system engineered with validation in mind is simpler to qualify, easier to document, and far less likely to trigger costly redesigns when the regulatory review comes back with questions. The plants that sail through IQ/OQ/PQ aren't lucky. They were designed for it from the beginning.
Q5) The Plant You Need in 2030 Is Being Decided Today
The business you're building this plant for today isn't necessarily the business you'll be running in five years. A well-engineered system anticipates that. It leaves room, in capacity, in utilities, in layout, for the process to evolve without requiring the plant to be torn apart and rebuilt.
Scalability is easy to overlook when the immediate priority is just getting the plant running. But the manufacturers who ask this question upfront are the ones who expand without pain later, instead of discovering, right when demand is finally growing, that their own plant is the bottleneck.
The Real Lesson: Plants Aren't Just Built. They're Engineered.
If there's one idea worth taking away from all five questions, it's this: good plants are not just built, they are engineered before they are built. Fabrication and installation are where a plant becomes physical. But the thinking that determines whether it actually works happens earlier, at the process and engineering stage.
This is the philosophy Propack Technologies brings to every project, working with manufacturers from process understanding and engineering, through manufacturing, automation, testing, and commissioning. Not just supplying equipment, but helping shape the decisions that determine how well that equipment performs for years to come.
Planning a New Facility or Expansion?
If you're at the stage of finalizing equipment for a new facility or expansion, it's worth pausing here first. Let's discuss your process requirements before you lock in your equipment, because the right conversation now can prevent a costly redesign later.
Propack Technologies, Engineering Solutions That Enrich Human Lives.


